Fiberglass reinforced plastic piping is stronger and more corrosion-resistant than most engineers initially expect. That's why getting the expansion joints right demands so much care.

Walk through any major industrial facility, such as a chemical plant, a municipal water treatment plant, a coal-fired power station’s scrubber system or a pulp and paper mill, and you will almost certainly encounter fiberglass reinforced plastic (FRP) piping. Since the 1940s, FRP has steadily displaced metal pipe in corrosive, demanding applications where stainless steel and exotic alloys are either too expensive or inadequate. Today it handles everything from various corrosive chemical processes, sulfur dioxide slurries in flue-gas desulfurization systems to potable water in municipal distribution networks.
The attributes driving FRP adoption are well documented: outstanding chemical resistance, exceptional strength-to-weight ratio, low maintenance costs a 70-year track record of standards development by ASTM, ASME, API, ISO AWWA. What is less consistently understood what generates a disproportionate share of piping system failures, is improperly supported piping and how to properly specify and install expansion joints within an FRP system.
Why FRP demands a different expansion joint mindset
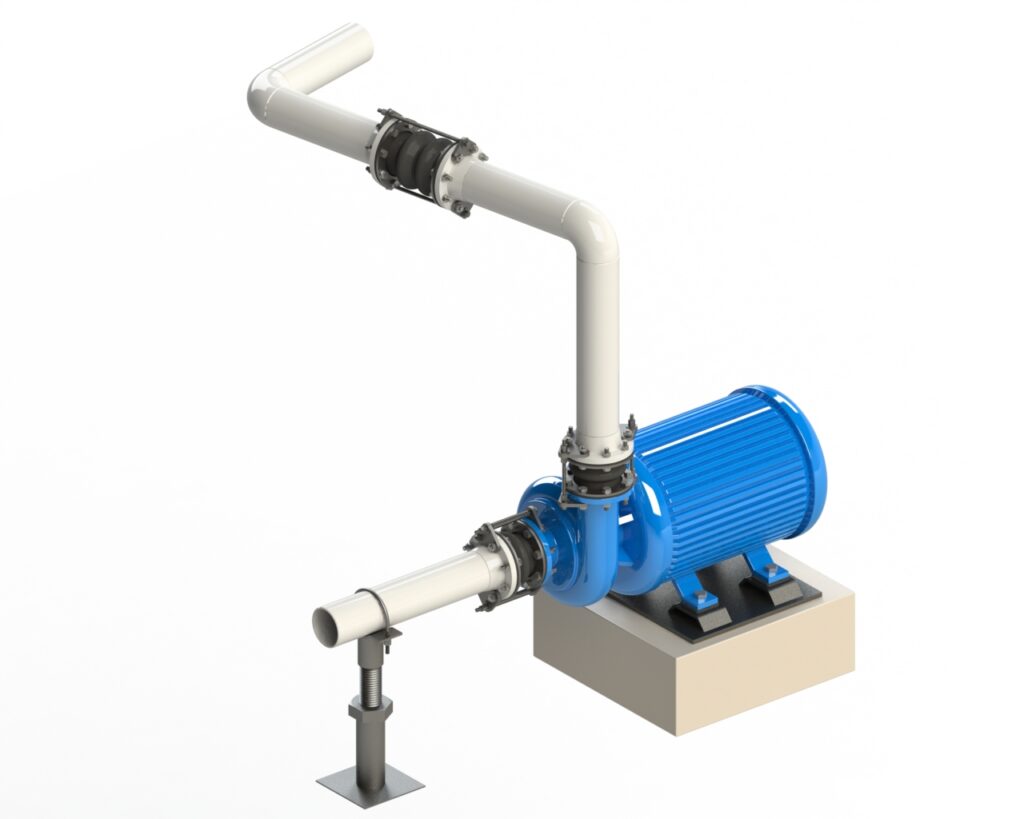
Expansion joints are flexible connectors designed to absorb movement caused by thermal expansion and contraction, pressure surges, vibration equipment-induced deflection. In a steel piping system, the designer selects an expansion joint capable of handling the forces generated by a strong stiff pipe. The logic is straightforward: everything is relatively rigid the joint must be robust enough to manage the loads.
FRP inverts that logic. The pipe itself, while strong in absolute terms, has a lower modulus of elasticity than carbon or stainless steel. More critically, FRP pipe expands at roughly twice the axial rate of steel due to its filament-wound construction, while its hoop-direction expansion is comparable. The result is that FRP systems generate lower thermal forces but larger thermal displacements than metal systems of the same dimensions. An expansion joint that is appropriately stiff for a steel system can, in an FRP system, effectively transfer load back into the flanges and pipe walls with potentially disastrous results.
The governing principle is counterintuitive to engineers who have spent their careers with metal pipe: the expansion joint must be the weakest mechanical element in the assembly. It must compress, extend or deflect before the pipe flange yields. Achieving that requires a deliberate reduction in joint stiffness, which means engineering expansion joints to a lower spring rate than would ever be acceptable in a steel system.
The STAMPED framework: Don’t shortcut the data gathering
The single most common cause of expansion joint failure in FRP systems is not a manufacturing defect or a material incompatibility; it is an incomplete specification. Engineers under scheduling pressure submit abbreviated requests for quotation, receive a standard joint recommendation install it. When the system enters service and fails prematurely, the root cause usually traces back to data that was never provided.
The industry has long used the STAMPED acronym as a data-collection framework it deserves more rigorous application in FRP projects than it typically receives. Be sure to collect the following data:
Size: Inner pipe diameter, wall thickness overall face-to-face distance all affect expansion joint geometry. FRP pipe varies more in wall thickness across manufacturers than steel pipe does. This matters.
Temperature: The full temperature range, not just the design operating temperature. The delta between the installation temperature and the operational extremes drives expansion and contraction calculations. What is the minimum ambient temperature during the winter shutdown? What is the maximum process upset temperature?
Application: Industry, media type (liquid, gas, slurry) pH. FRP’s resin system is selected for specific chemical exposures the expansion joint elastomer must be compatible with the same media. For abrasives flowing through the system, it is important to match identification of expansion joint to the pipe
Movement: Type, direction magnitude. Axial compression and extension, lateral offset angular deflection each impose different demands on the joint. All three can occur simultaneously. Use a concurrent movement calculator.
Pressure/Vacuum: Operating, test surge pressures. FRP systems often operate at lower pressures than metal systems, but water hammer and surge events are unforgiving.
End Fittings: Flange drilling pattern, backing ring configuration whether the FRP flange is solid laminate, overlay or stub-end. The joint must distribute bolt load across the full flange face without point-loading a relatively brittle composite rim.
Delivery: Lead time affects both the manufacturing process and the temptation to substitute a standard stock joint for a custom-engineered one. Plan accordingly.
Calculating thermal movement: FRP is not steel
The filament-wound structure of FRP pipe creates anisotropic thermal behavior, meaning the material expands at different rates in different directions. In the hoop (circumferential) direction, FRP’s coefficient of thermal expansion approximates that of steel. In the axial direction, it is approximately twice that of steel.
For long pipe runs, which are common in industrial facilities, this axial differential is significant. The expansion joint specification must account for the full thermal excursion: from the installation temperature to the maximum design temperature for expansion from the installation temperature to the minimum design temperature for contraction. Both directions must be within the joint’s rated range of motion, with an appropriate safety margin.
Many projects also require a pipe stress analysis, either through computer modeling or manual calculations, to determine the actual forces and movements at each joint. This analysis drives the allowable spring rate i.e., the force per unit of deflection, the joint is permitted to impose on the system. For FRP, the allowable is typically well below what would be acceptable in steel, making the stress analysis not a formality but a genuine design constraint.

Installation: Alignment, preset support
Even a correctly specified joint can fail if installed improperly. FRP pipe and fittings require careful alignment; industry practice recommends maintaining alignment to within 1/8 inch at the joint. Lateral misalignment beyond that threshold imposes immediate lateral load on the joint and, more importantly, on the FRP flange.
Preset, the practice of partially compressing or extending a joint during installation to center its movement range around the operating condition, is often necessary in FRP systems. Because FRP pipe generates larger axial movements than metal pipe, a joint installed at its neutral position may be unable to accommodate the full operational excursion in one direction. The degree of preset must be calculated based on the installation temperature relative to the expected operating range.
Pipe supports in FRP systems must be designed to prevent lateral movement while allowing axial movement at expansion joint locations. Guides and anchors carry forces that the pipe itself may not be able to bear, making load-path design as important as joint selection.

Engage early, engage deeply
The consistent message from facilities that have successfully operated FRP systems for decades is that expansion joint selection is not a procurement task; it is an engineering collaboration. Engaging expansion joint manufacturers and FRP piping specialists early in the design process, before pipe routing and support locations are finalized, enables the entire system to be optimized. Changes to joint placement, pipe routing or support spacing are far less expensive at the design stage than as retrofits after a field failure.
Knowledgeable suppliers can review pipe stress analysis outputs, recommend specific joint types and spring rates for each location flag installation issues before they become problems. Industry associations such as the Fluid Sealing Association provide standards and guidance that manufacturers contribute to and apply in practice.
Rob Coffee is the vice president of sales and marketing for Proco Products.